Vacuum Casting vs Injection Molding: How to Choose for Your Proj
Vacuum casting and injection molding can both produce repeat plastic parts, but they support different stages of product development and different purchasing requirements. The right choice depends on design maturity, target quantity, material performance, cosmetic requirements, tolerance needs, and the cost of tooling.
Vacuum casting is commonly selected for prototype sets, engineering validation parts, customer samples, and low-volume bridge production. Injection molding is generally more suitable when the design is stable, production-grade thermoplastic properties are required, and the expected demand can justify metal tooling.
This guide explains how to compare the two processes before committing to a manufacturing route. It is intended for engineers, product developers, OEM buyers, and project managers who need to balance development risk, cost, delivery planning, and part performance.

Vacuum Casting vs Injection Molding: The Decision in One View
The key difference is the tooling. Vacuum casting uses silicone molds, usually made from a CNC-machined or SLA-printed master pattern. Injection molding uses a metal tool that is designed to withstand repeated cycles of molten thermoplastic under pressure.
Silicone tooling is generally faster and less expensive to prepare, making it useful when the design is still being evaluated or when only a limited number of parts are needed. Metal tooling requires more up-front planning and investment, but it supports repeatable production over much higher volumes.
| Decision Factor | Vacuum Casting | Injection Molding | What It Means for the Project |
|---|---|---|---|
| Tooling type | Silicone mold | Metal mold, commonly aluminum or steel | Tooling type affects initial cost, modification effort, and production life |
| Typical project stage | Prototype, engineering validation, pilot build, bridge production | Stable product design, pilot production, recurring production demand | Design maturity should be reviewed before selecting a process |
| Up-front tooling commitment | Usually lower | Usually higher | Important when the design may still change after testing |
| Suitable quantity | Often used for low-volume part requirements | More suitable as volume and repeat demand increase | Quantity should be reviewed together with design stability and tooling budget |
| Material system | Polyurethane-based casting resins | Production-grade thermoplastics and selected engineering polymers | Material performance requirements can determine the correct process |
| Design changes | Generally easier to accommodate before new silicone molds are made | Tool changes may add cost and time after metal tooling is produced | Useful for projects still undergoing engineering refinement |
| Surface finish | Can reproduce master-pattern texture and cosmetic details | Can reproduce mold texture consistently over larger production volumes | Visible surfaces should be defined before tooling begins |
| Long-run unit cost | May increase as quantities grow and molds require replacement | Can become more favorable when tooling is amortized across higher volumes | Total project cost matters more than piece price alone |
Choose Vacuum Casting When Design Validation Is Still Needed
Vacuum casting is often a practical route when the product design is close to completion but still requires assembly checks, appearance review, functional handling tests, customer feedback, or limited pilot use. The process supports multiple similar parts without requiring permanent production tooling at the earliest stage.
For example, a product team may need 20 enclosure sets to verify screw locations, internal mounting posts, cable openings, fit with electronics, and visible surface appearance. In that situation, producing silicone molds can be more appropriate than investing in injection tooling before the final design has been verified.
Choose Injection Molding When Volume and Material Requirements Are Confirmed
Injection molding becomes more suitable when the part design is stable, demand is recurring, and the product requires the intended production thermoplastic. This may include applications that need a defined resin grade, higher heat resistance, specific chemical resistance, long-term mechanical performance, or repeatable production across a larger order volume.
Injection molding can also be the stronger option when dimensions are highly critical, when the project requires long-run repeatability, or when unit cost must be optimized over a large production schedule. The decision should be based on the complete manufacturing plan rather than a single target quantity.
Tooling Cost, Part Cost, and Total Project Cost
Comparing only the price per part can lead to the wrong manufacturing decision. A project should instead compare the total cost of the required parts, including master-pattern preparation, silicone or metal tooling, secondary operations, inspection, design-change risk, and the expected next production stage.
Why Silicone Tooling Reduces Early-Stage Commitment
Vacuum casting begins with a master pattern and silicone mold rather than a durable metal tool. This route can reduce early tooling commitment when the design is not fully frozen. If engineering feedback identifies a change to a wall thickness, mounting feature, opening, boss, logo, or visible surface, it may be more practical to revise the master pattern and mold than to rework metal tooling.
This is why vacuum casting is frequently used as a bridge between one-off prototypes and injection molding. It allows product teams to review a set of parts that more closely represent a molded product while preserving flexibility for further design changes.
Why Injection Molding Can Improve Cost at Higher Volumes
Metal tooling requires higher up-front investment, but its longer production life can make injection molding more economical when demand is stable and volume is sufficiently high. The tool can be used for repeated production cycles, which supports lower unit cost over time when the initial tooling expense is spread across many parts.
However, a lower unit cost does not automatically mean a lower project cost. If a design change is likely after the tool is made, the cost and schedule impact of mold modification should be considered before the initial tooling decision is approved.
How Design Changes Affect Each Manufacturing Route
Design changes are common during prototype development. A part may need a larger opening, stronger mounting boss, revised connector location, thicker wall, different texture, or improved assembly clearance after the first build.
- Vacuum casting can be appropriate when part geometry may continue to change after prototype testing.
- Injection molding is more suitable when the product design, resin, assembly interfaces, and production requirement are substantially confirmed.
- Critical changes should be identified before any tooling route is selected, especially changes that affect parting lines, draft, ribs, undercuts, wall thickness, and cosmetic surfaces.
- Purchasing teams should request a manufacturing review before approving tooling when the project includes tight dimensions, inserts, snap fits, or visual requirements.
Production Quantity and Timeline Planning
Quantity matters, but it should not be used as a fixed rule without considering the project stage. The same order quantity can require different manufacturing routes depending on whether the parts are for early testing, customer demonstration, pilot production, or stable recurring demand.
Prototype and Bridge Production Requirements
Vacuum casting is often used for prototype sets and low-volume production because silicone molds can produce repeat parts without the up-front commitment of injection molds. A single silicone mold has a limited working life, so projects requiring more parts may need multiple molds or a different process route.
For many projects, the useful question is not simply “How many parts are needed?” but “How many identical parts are needed before the next likely design revision?” If the answer is limited and the design is still evolving, vacuum casting can be a practical option.
When Multiple Silicone Molds May Be Considered
When the required quantity exceeds the output of one mold, a manufacturer may evaluate whether to create additional silicone molds. This can support larger low-volume programs, but the project should be reviewed for total cost, material requirements, dimensional consistency, appearance standards, and expected future demand.
Part size, geometry, wall thickness, undercuts, resin type, demolding force, and finishing requirements all affect silicone mold life. For this reason, the exact output per mold should be confirmed after the part design is reviewed rather than assumed from a general estimate.
When Metal Tooling Should Enter the Production Plan
Metal tooling should be evaluated when the design is stable and the project requires higher output, repeat production, or production-grade material performance. It is also appropriate to review injection molding when the product will be sold or used in environments that require the properties of a specified thermoplastic rather than a polyurethane material simulation.
For a project moving from prototype to production, the transition may include more than one step. A development team may first validate appearance and assembly through vacuum cast parts, then produce pilot parts with prototype tooling, and later move to production injection molds after design and demand are confirmed.
Material Performance and Part Function
Material requirements are among the most important factors in the vacuum casting versus injection molding decision. Although polyurethane casting resins can simulate the appearance or feel of common plastics, they are not automatically equivalent to the exact thermoplastic resin intended for mass production.
Polyurethane Casting Materials and Material Simulation
Vacuum casting typically uses polyurethane resins formulated to create rigid, flexible, rubber-like, transparent-like, colored, or engineering-plastic-like parts. These materials can be useful for product development, fit testing, appearance review, handling evaluation, and selected functional tests.
Material selection should be tied to the purpose of the prototype. A housing intended for assembly testing may require rigidity and cosmetic consistency, while a grip component may need flexible or rubber-like behavior. A buyer should state the intended use, expected loading, temperature range, chemical exposure, and test requirements before material selection is confirmed.
When Production-Grade Thermoplastic Properties Are Required
Injection molding is usually the more appropriate process when a project requires the exact performance of the final production resin. This can apply when the part must meet defined requirements for heat resistance, impact performance, chemical resistance, electrical behavior, flame rating, regulatory documentation, or long-term environmental exposure.
For example, a prototype enclosure can be vacuum cast for fit, appearance, and internal assembly checks. However, if the final product must pass a specific thermal, electrical, chemical, or regulatory test using a named production resin, injection molding or another material-appropriate prototype process may need to be evaluated.
Environmental and Mechanical Performance Considerations
- Use vacuum casting when the project needs low-volume parts for appearance, fit, handling, assembly, or selected functional evaluation.
- Review injection molding when the final thermoplastic grade and its production behavior must be verified.
- Identify exposure to heat, UV light, moisture, chemicals, repeated loading, impact, or outdoor environments before selecting the casting material.
- Confirm whether the part is a visual prototype, a functional test part, a temporary field-evaluation unit, or an end-use production component.
- Include material documentation, testing, traceability, or regulatory requirements in the project brief when they are mandatory.
Surface Finish, Appearance, and Assembly Requirements
Both processes can produce parts with controlled cosmetic features, but the route to the final appearance differs. In vacuum casting, the surface condition of the master pattern has a direct influence on the silicone mold and the resulting casting. In injection molding, the tool surface, texture, gate location, and process settings affect the finished part appearance.
Cosmetic Appearance for Prototype and Presentation Samples
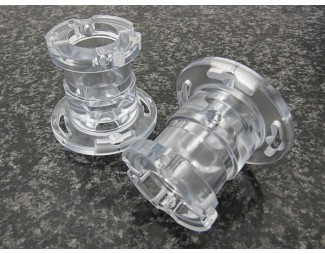
Vacuum casting can be suitable for prototype enclosures, housings, covers, bezels, grips, and product samples that require a molded appearance. Silicone molds can reproduce texture and visible details from the master pattern, making master-pattern preparation important for surface quality.
For customer demonstration samples, the project should define visible surfaces, color expectations, texture, gloss level, paint requirements, logo treatment, and acceptable gate or parting-line locations before mold production begins.
Textures, Colors, Logos, and Visible Surfaces
Surface features should be reviewed early because they affect both the master pattern and the post-processing route. Fine textures, engraved logos, raised lettering, paint, color matching, and high-gloss surfaces may require additional planning to achieve a consistent result across a set of prototype parts.
- Identify Class A or customer-visible surfaces on the drawing or CAD model.
- Confirm whether a matte, textured, gloss, painted, or natural cast finish is required.
- State whether color must match a sample, Pantone reference, RAL reference, or internal brand specification.
- Place parting lines and gates away from key visible areas where possible.
- Review whether logos, text, labels, or fine markings need to be molded, painted, or applied after casting.
Threads, Inserts, Snap Features, and Mating Dimensions
Assembly features should be reviewed as functional requirements rather than treated as secondary details. Screw bosses, threaded inserts, clip features, snap fits, pins, holes, and mating surfaces may need design adjustments depending on the selected manufacturing route and the required level of repeatability.
For vacuum cast parts, critical assembly features should be clearly marked in the 2D drawing. This helps the manufacturing team identify which dimensions need additional attention during mold planning, post-processing, or inspection. For injection molding, draft, wall thickness, steel-safe conditions, and tool-access requirements should be addressed before the tool is built.
Design Changes and Engineering Risk Before Tooling
The most expensive manufacturing decision is often not choosing the wrong process at the beginning. It is committing to permanent tooling before the design, functional requirements, and demand forecast are sufficiently confirmed.
Why Design Maturity Matters Before Committing to Injection Molds
Injection molds are developed around a defined part design. Changes to a part after tooling may affect the mold cavity, core, slides, inserts, gates, cooling, ejection, or texture. Some changes are relatively manageable, while others can require significant rework or tool replacement.
A product should therefore be evaluated for design maturity before injection tooling is approved. This includes geometry, material, wall thickness, draft, assembly interfaces, cosmetic expectations, expected production volume, and potential future product revisions.
Features That Should Be Verified During Prototype Builds
- Fit with mating components, electronics, seals, fasteners, and internal hardware
- Access to buttons, connectors, displays, cables, and assembly tools
- Strength and placement of mounting posts, clips, ribs, and brackets
- Wall thickness transitions and areas that may affect deformation or appearance
- Clearance for moving parts, covers, latches, and removable panels
- Surface appearance under the expected lighting and customer review conditions
- Packaging, handling, shipping, and field-use considerations
How to Document Critical Dimensions and Acceptance Requirements
Not every dimension requires the same level of control. A project should identify dimensions that are critical to assembly, sealing, function, safety, appearance, or customer acceptance. These features should be clearly marked in the drawing and discussed during the manufacturing review.
Other requirements should also be documented, including surface finish, color, texture, insert locations, inspection points, packaging needs, and target delivery date. Clear documentation reduces uncertainty for both the purchaser and the manufacturer.
Selection Matrix for Common Project Scenarios
| Project Scenario | More Suitable Starting Route | Why | What to Confirm Before Proceeding |
|---|---|---|---|
| One functional prototype with critical threads or tight mating features | CNC machining or another process based on material need | Can support precise functional features and specified materials | Material, tolerance, thread specification, and required test conditions |
| Several enclosure samples for assembly and appearance review | Vacuum casting | Supports repeat prototype sets without permanent metal tooling | Quantity, visible surfaces, color, texture, and critical mounting features |
| Customer samples before the product design is frozen | Vacuum casting or SLA, depending on quantity and finish needs | Allows feedback before committing to injection tooling | Cosmetic standard, delivery schedule, and expected design changes |
| Pilot build with a stable design and recurring demand forecast | Evaluate injection molding | May better support planned production material and repeatability | Annual volume, target resin, tool budget, and launch schedule |
| High-volume product with established material specification | Injection molding | Metal tooling supports repeated production cycles and lower long-run unit cost | Tool design, resin grade, quality plan, and production forecast |
Typical Project Example: Moving from Prototype Parts to Production Tooling
An industrial equipment manufacturer needed a set of plastic enclosure components for engineering validation and customer review. The enclosure included visible exterior surfaces, internal mounting posts, cable openings, and screw-boss features that had to align with electronic components and mating covers.
Buyer Requirement: The buyer required multiple parts for assembly testing before approving permanent production tooling. The design was close to final, but the project team still needed to confirm internal clearances, fastener positions, visible surface quality, and the location of control-panel cutouts.
Manufacturing Route Evaluation: ABC Rapid reviewed the part geometry, quantity requirement, critical interfaces, cosmetic surfaces, and expected next design review. Because the project required a limited set of parts before design freeze, a silicone mold vacuum casting route was evaluated for prototype production. The review also identified which features should be verified before a later injection molding tool was considered.
Result: The project team could assess assembly, appearance, and functional interfaces using repeat prototype parts before committing to permanent tooling. After engineering feedback was incorporated, the buyer had a clearer basis for deciding whether to continue with low-volume cast parts or move toward injection molding for future demand.
FAQ: Vacuum Casting vs Injection Molding
Is vacuum casting cheaper than injection molding?
Vacuum casting often has a lower initial tooling commitment because it uses silicone molds rather than permanent metal tools. Injection molding may provide a lower long-run unit cost when the tooling cost is distributed across a larger, stable production volume. The correct comparison should include total project cost, expected quantity, design-change risk, material needs, and future demand.
What quantity makes injection molding more suitable?
There is no single quantity that applies to every part. Injection molding becomes more attractive when the design is stable, demand is recurring, and the cost of metal tooling can be justified over the planned production volume. Part size, geometry, resin, cavity count, quality requirements, and expected future orders all affect the decision.
Can vacuum cast parts be used for functional testing?
Yes, vacuum cast polyurethane parts can be used for fit checks, assembly validation, handling assessment, appearance review, and selected functional testing. However, if the test requires the exact properties of the final production thermoplastic, injection molding or another process using the intended material should be evaluated.
Can vacuum casting reproduce injection-molded surface textures?
Vacuum casting can reproduce the texture and surface details of the master pattern through the silicone mold. The final appearance depends on master-pattern quality, mold preparation, resin selection, color treatment, post-processing, and the defined cosmetic acceptance standard.
Should I validate assembly before ordering injection molds?
In most cases, assembly features such as mounting posts, holes, fastener locations, clips, clearances, cable routing, and mating interfaces should be reviewed before permanent tooling is approved. Prototype parts can help identify issues that would be more costly to change after injection mold production begins.
Can a vacuum casting company support a project before injection molding?
A vacuum casting company can support the prototype and bridge-production stage by reviewing CAD models, material behavior, visible surfaces, target quantity, and critical assembly features. For projects that later move to higher volumes, the information gained from prototype builds can help prepare a more complete injection molding specification.
Review the Right Manufacturing Route Before Tooling Commitment
Vacuum casting and injection molding are not competing processes in every project. In many product development programs, vacuum casting supports design validation and low-volume needs before injection molding is used for stable production. The best route depends on what the parts must prove, how many are required before the next design change, and whether the project needs simulated or production-grade material performance.
For prototype sets, bridge production, and silicone mold evaluation, review vacuum casting services for prototype and low-volume parts. ABC Rapid can review drawings, material expectations, quantity, critical dimensions, visible surfaces, and delivery requirements before a production route is selected.
Buyers comparing supplier capabilities may also evaluate a vacuum casting factory for custom prototype parts when a project requires repeat polyurethane components, silicone tooling, and engineering review before production tooling is justified.
For projects that have moved beyond prototype validation and require repeat production using specified thermoplastic materials, review injection molding options for recurring production parts.
When appearance requirements include paint, color, texture, or cosmetic finishing, see surface finishing options for prototype parts.
Search
Recent Post


Other New Articles